Ekontrol Engineering Practicum in Yaremche: ISO 22002-100:2025 and FSSC 22000 Workshop Outcomes for FSTs
On January 28, 2025, the Ekontrol lead auditor and engineering team hosted an intensive offsite practicum in Yaremche dedicated to the structural overhaul of the ISO 22002:2025 series and its direct impact on FSSC 22000 certification audits. Rather than running a slide-based lecture, we built the event as a hands-on engineering workshop for active Food Safety Teams (FSTs): quality directors, chief technologists, chief engineers, sanitation managers, laboratory heads, and internal auditors from food processing, packaging, feed, and cold-chain logistics enterprises.
Why did this structural reform require an immediate engineering response? Technical committee ISO/TC 34/SC 17 replaced the standalone technical specifications ISO/TS 22002-1:2009, ISO/TS 22002-2:2013, ISO/TS 22002-4:2013, ISO/TS 22002-5:2019, and ISO/TS 22002-6:2016 with full international standards anchored by the umbrella standard ISO 22002-100:2025. Most manufacturing sites still operate with prerequisite programs (PRPs) drafted around legacy ISO 22002-1:2005 or ISO/TS 22002-1:2009 clauses. Those older documents don't match the new two-tier structure or the latest benchmarking criteria enforced by the Global Food Safety Initiative (GFSI).
Why Standard Classroom Lectures Fail Food Safety Teams
When a quality manager attends a routine webinar from their desk at the plant, operational emergencies interrupt them every twenty minutes. A raw material truck arrives with a broken seal, a filler line stops for unplanned sanitation, or a buyer requests an urgent specification update. Training notes end up in a drawer while shop-floor PRP procedures remain untouched for months. Pulling multidisciplinary teams out of daily plant firefighting to Yaremche solved that problem.
Before arriving at the workshop, participating teams assembled real technical dossiers from their facilities: master PRP matrices, architectural zoning blueprints, air handling (HVAC) schematics, Clean-in-Place (CIP) validation logs, Environmental Monitoring Program (EMP) swabbing maps, and nonconformity reports from recent surveillance audits. Over the course of the session, each team ran a clause-by-clause gap analysis of their own documentation, exposed blind spots between maintenance and quality departments, and built a practical schedule for upgrading their ISO 22000 food safety management system.
Honestly, the biggest realization for many participants was that the highest risks during the ISO 22002-100:2025 transition sit in physical plant utilities and missing metrological proof, not in document numbering. When a chief engineer and an FST leader examine floor drain gradients or air pressure differentials across a high-care packaging wall together, years of departmental friction disappear in minutes.
The Dual-Standard Audit Rule Practiced During the Yaremche Workshop
During the Yaremche practicum, participating teams practiced the core regulatory rule of the 2025 architecture: the umbrella standard ISO 22002-100:2025 cannot be used on its own. During an FSSC 22000 certification audit, the auditor verifies an inseparable pair of standards: all 18 common clauses of ISO 22002-100:2025 combined with your sector-specific standard (ISO 22002-1:2025 for Category C, ISO 22002-4:2025 for Category I, or ISO 22002-5:2025 for Category G). If your PRP matrix doesn't cross-reference both tiers, certification bodies record a systemic nonconformity under Clause 8.2 of ISO 22000.
Two-Tier Architecture of ISO 22002-100:2025 and Sector Standards (-1, -4, -5): Practical Breakdown
The opening module of the Yaremche training unpacked the structural shift from legacy specifications (ISO 22002-1:2005 / PAS 220 / ISO/TS 22002-1:2009) to the two-tier ISO 22002:2025 series. Under the old system, every link in the food supply chain had a separate specification where 75-80% of the text repeated identical baseline rules for building layout, pest control, personal hygiene, waste handling, and chemical storage. Meanwhile, wording differences across those separate documents created headaches for multi-site groups regarding allergen control, cross-contamination, and supplier approval.
In the new architecture, all universal prerequisite requirements sit inside the common umbrella standard ISO 22002-100:2025, harmonized with the General Principles of Food Hygiene of Codex Alimentarius (CXC 1-1969, 2020/2022 revision). The sector parts (ISO 22002-1:2025, ISO 22002-2:2025, ISO 22002-4:2025, ISO 22002-5:2025, ISO 22002-6:2025, and ISO 22002-7:2025) now contain only process-specific engineering controls for each respective supply chain category.
How Teams Restructured PRP Documentation Without Paper Bloat
We split participants into working groups by industry category and gave them a concrete engineering assignment: migrate existing PRP manuals to the dual-standard format without creating dozens of redundant standard operating procedures (SOPs). Teams worked through six practical tasks:
- SOP De-duplication Across Multi-Site Operations: consolidating the 18 universal clauses of
ISO 22002-100:2025into a single corporate baseline manual for vertically integrated groups operating processing plants, warehouses, and transport fleets. - Sector Add-Ons Under
ISO 22002-1:2025(Category C): specifying hygienic equipment design, sanitation validation, foreign body prevention (metal detectors, X-ray inspection, sifters, neodymium magnetic traps with induction $\ge 10,000\text{ Gauss}$), and rework segregation. - Food Packaging Controls Under
ISO 22002-4:2025(Category I): replacing legacyISO/TS 22002-4:2013references with strict verification of chemical migration, printing inks, photoinitiators, adhesives, and residual solvents. - Transport and Cold-Storage Controls Under
ISO 22002-5:2025(Category G): defining 3D thermal mapping for warehouses and reefers, dock-door discipline, cross-docking hygiene, and tanker washout verification. - Integration With ISO 22000 and HACCP Hazard Analysis: drawing a sharp boundary between baseline
PRPs, operational prerequisite programs (OPRPs), and critical control points (CCPs) under the official FSSC 22000 scheme. - Unannounced Audit Evidence Design: building shift verification checklists that operators can complete in three minutes while generating an indisputable audit trail.
The engineering table below summarizes the cross-sector mapping matrix compiled by teams during the Yaremche practicum.
| Supply Chain Sector and FSSC 22000 Category | Legacy Specification (Pre-2025) | New Paired Architecture (ISO 22002:2025) | Yaremche Workshop Case Focus | Typical Audit Gap Identified by Participating Teams |
|---|---|---|---|---|
| Food Manufacturing (Category C: C0, CI, CII, CIII, CIV) | ISO 22002-1:2005 (early editions) and ISO/TS 22002-1:2009 | ISO 22002-100:2025 + ISO 22002-1:2025 | Hygienic zoning, HVAC pressure cascades, CIP validation, allergen changeover, floor drainage direction | No instrumental differential pressure logs between zones and visual-only sign-off after line sanitation |
| Food Packaging and Container Manufacturing (Category I) | PAS 223:2011 and ISO/TS 22002-4:2013 | ISO 22002-100:2025 + ISO 22002-4:2025 | Overall (OML) and specific (SML) migration testing, NIAS screening, functional barriers, ink set-off in reels | Supplier Declarations of Compliance lack ISO/IEC 17025 lab test reports in appropriate food simulants |
| Transport, Cold Chain, and Storage Logistics (Category G) | ISO/TS 22002-5:2019 | ISO 22002-100:2025 + ISO 22002-5:2025 | 3D reefer thermal mapping, cross-docking temperature recovery, EFTCO tanker cleaning certificates, load security | Temperature data loggers mounted only near evaporator outlets without monitoring the warmest spot near rear doors |
| Animal Feed and Premix Manufacturing (Category D) | PAS 222:2011 and ISO/TS 22002-6:2016 | ISO 22002-100:2025 + ISO 22002-6:2025 | Mixer homogeneity validation (CV <= 5%), medicated feed carry-over prevention, sequencing and flushing | Flushing batches used between medicated and non-medicated runs without quantitative lab verification of active residue |
| Catering, Food Service, Retail, and Wholesale (Categories E, F) | ISO/TS 22002-2:2013 and local hygiene codes | ISO 22002-100:2025 + ISO 22002-2:2025 / ISO 22002-7:2025 | Blast-chilling kinetics (+60 °C to +10 °C <= 2 hours), display cabinet cold chain, FEFO stock rotation | Manual temperature checks recorded twice per shift with no automated alarm logging during peak defrost cycles |
Shop-Floor Case Studies (Category C): Hygienic Zoning, HVAC Positive Pressure, and CIP Validation Under ISO 22002-1:2025
The most intense technical debates during the Yaremche group sessions centered on ISO 22002-100:2025 and ISO 22002-1:2025 requirements for food processing facilities (dairies, meat processing plants, bakeries, confectionery lines, and beverage bottlers). Each group had to defend a real plant layout and sanitation protocol in front of an audit panel made up of Ekontrol lead auditors and engineers from peer companies.
Case 1: Hygienic Zoning, Traffic Segregation, and HVAC Positive Pressure Cascades
When reviewing an actual floor plan for a Ready-to-Eat (RTE) dairy packaging hall, participants spotted a classic architectural flaw: pallets of outer corrugated cardboard crossed the same corridor used by operators entering the High Care / High Hygiene zone after changing boots and coveralls. Under older practices, the plant tried to manage that hazard through time separation on a schedule. However, ISO 22002-100:2025 (Clause 5) and ISO 22002-1:2025 demand physical barrier segregation and complete elimination of intersecting paths between raw materials, finished exposed products, waste, and outer packaging.
Working alongside plant engineers, teams calculated the aerodynamic barrier required from the heating, ventilation, and air conditioning (HVAC) system. Preventing unfiltered air from being sucked from medium-hygiene or ambient corridors into open-product filling rooms requires a continuous positive static pressure differential:
$$\Delta P = P_{\text{high care}} - P_{\text{medium hygiene}} \ge 5\text{-}15\text{ Pa}$$
During the workshop, teams drafted concrete engineering specifications for their maintenance departments:
- installing Magnehelic differential pressure gauges (or digital pressure transmitters linked to SCADA) directly at airlock doors between zones with visual alarms if doors stay propped open;
- equipping clean-zone air handling units with multi-stage filtration rated at
F7-F9(ISO 16890ePM1 55-80%) and terminalHEPA H13/H14filters (EN 1822), replacing filter cassettes based on maximum pressure-drop thresholds rather than arbitrary six-month calendar dates; - controlling indoor dew-point temperature ($T_{\text{dew}}$) in chilled processing rooms so condensation never forms on ceiling panels, overhead ducts, or evaporator fins, eliminating a primary vector for Listeria monocytogenes droplets;
- configuring floor drainage channels with trapped gullies and backflow preventers so effluent flows strictly from
High CaretowardBasic Hygieneareas at a floor slope of1.5-2.0%without standing puddles.
Case 2: Engineering Validation of Clean-in-Place (CIP) Circuits Using Sinner's Circle
Our second shop-floor case examined closed-circuit CIP sanitation records. Across FSSC 22000 audits, more than 40% of sanitation nonconformities happen because Food Safety Teams confuse daily operational monitoring with initial engineering validation and periodic verification. In Yaremche, teams applied Sinner's Circle parameters (fluid mechanics, thermal energy, chemical concentration, contact time) to their own CIP logs and uncovered three frequent engineering failures:
- Velocity Drop in Stepped-Diameter Piping: if a centrifugal pump drives caustic wash liquid through a
DN 50pipe at $v = 1.8\text{ m/s}$, expanding that same flow into aDN 80manifold drops linear velocity inversely with the square of pipe diameter down to $v \approx 0.7\text{ m/s}$. At that speed, the Reynolds number ($Re = \frac{v \cdot D}{\nu}$) falls below the turbulent scrubbing threshold ($Re < 25,000$), leaving boundary-layer biofilm intact regardless of caustic temperature. - Measuring Dosing Pump Strokes Instead of Return-Line Conductivity (
CIP Return): caustic soda (NaOHat1.5-2.2%and68-75 °C) and nitric or phosphoric acid (HNO3at0.8-1.2%and55-65 °C) must be controlled via temperature-compensated conductivity sensors mounted on theCIP Returnline, backed up by manual acid-base titration in the plant laboratory. - Dead Legs and Spray-Ball Shadow Zones: under
EHEDGhygienic design rules, any T-piece or instrument branch must maintain a length-to-diameter ratio of $L/D < 1.5$ (and never above $2.0$). Participants practiced documenting riboflavin fluorescence spray tests under365 nmUV light to verify 100% wetting of tank domes, agitator shafts, and manway gaskets during equipment commissioning.
Packaging Migration (ISO 22002-4:2025), Allergen Swabbing, EMP Zoning (Zones 1-4), and TACCP/VACCP Defense
A dedicated engineering module at the Yaremche practicum addressed sector requirements for packaging manufacturers (ISO 22002-4:2025) and logistics operators (ISO 22002-5:2025), alongside cross-cutting FSSC 22000 additional requirements: allergen changeover validation, Environmental Monitoring Programs (EMP), Food Defense (TACCP), and Food Fraud mitigation (VACCP).
Case 3: Packaging Migration, NIAS, and Printing Ink Set-Off Under ISO 22002-4:2025
Working with packaging converters and food-plant procurement specialists, we examined how ISO 22002-4:2025 tightens controls over primary food contact materials (flexible multilayer films, PET preforms, paperboard trays, and metal cans). Participants audited real Declarations of Compliance (DoC) from their current packaging suppliers and discovered that 65% of the files lacked migration test reports performed in the correct food simulants (Simulants A, B, C, D1, and D2 under EU Regulation 10/2011).
During the group exercise, teams built a technical verification protocol covering four mandatory parameters:
- verifying the Overall Migration Limit (
OML$\le 10\text{ mg/dm}^2$ of contact surface or $\le 60\text{ mg/kg}$ of food simulant) and Specific Migration Limits (SML) for monomers, plasticizers, antioxidants, and catalysts; - screening Non-Intentionally Added Substances (
NIAS), including polymer thermal degradation byproducts formed during high-temperature extrusion, oligomers, and contaminants in recycled polymers (rPET); - preventing invisible
set-offtransfer of low-molecular-weight UV ink photoinitiators and coatings from the printed outer surface onto the food-contact inner surface when flexible film is wound under high tension on slitter-rewinders; - running gas chromatography headspace tests for residual lamination solvents (ethyl acetate, methoxypropanol, isopropanol) in testing laboratories accredited to ISO/IEC 17025.
Case 4: Allergen Changeover Validation and the ATP Bioluminescence Misconception
In the allergen management workshop (updated Clause 12 of ISO 22002-100:2025, expanded in ISO 22002-1:2025 and FSSC 22000 Additional Requirement 2.5.6), we tackled a widespread misconception that trips up nearly half of food plants during certification audits. Several teams assumed that an ATP bioluminescence swab reading below 10-30 RLU after wet or dry line cleaning proved the absence of allergens such as milk casein, gluten, soy, peanut, hazelnut, or egg protein.
In Yaremche, we demonstrated why auditors reject that practice: ATP luminometers detect adenosine triphosphate from living or recently lysed cells and general organic soil, whereas allergenic proteins don't contain ATP and remain immunochemically active even after baking, roasting, or pasteurization. Validating a changeover from an allergen-containing recipe to a free-from product requires allergen-specific Lateral Flow Devices (LFDs with 1-5 ppm detection thresholds) for routine shift release and quantitative ELISA immunoassays across three consecutive production cleanings for formal method validation.
Case 5: Environmental Monitoring Program Zoning (EMP Zones 1-4) and TACCP/VACCP Drills
Next, teams mapped pathogen swabbing points onto their plant drawings under FSSC 22000 Additional Requirement 2.5.7 and ISO 22002-1:2025, dividing facilities into four concentric hygienic zones:
- Zone 1 (Direct Food Contact Surfaces post-lethality): slicer blades, depositor nozzles, conveyor belts, filling hoppers, and packaging chutes.
- Zone 2 (Adjacent Non-Food Contact Surfaces): equipment frames, operator touchscreens, drip pans underneath overhead evaporators, and exterior filler housings.
- Zone 3 (Remote Processing Room Surfaces): floor drains, P-traps, pallet-jack wheels, walls, door handles, and squeegees.
- Zone 4 (Areas Outside the Processing Room): locker rooms, maintenance workshops, raw-material warehouses, and corridors.
Teams drafted a Seek and Destroy escalation protocol whenever Listeria spp. or Salmonella spp. turns up in Zone 2 or Zone 3: vector swabbing within a 2-3 meter radius around the positive point, disassembling hollow rollers and gaskets to locate harborage niches, and executing deep chemical-thermal sanitation before the pathogen reaches Zone 1.
In parallel, during the TACCP (Food Defense) and VACCP (Food Fraud) tabletop exercise, participants tested physical security locks on outdoor bulk silos, CIP chemical cabinets, and water storage tanks, while writing mass-balance equations to catch economically motivated adulteration in high-risk ingredients (cocoa butter, olive oil, milk powder, spices).
Three High-Risk Audit Findings Teams Uncovered in Their Own Procedures
Reviewing actual plant procedures in Yaremche exposed three systemic vulnerabilities that trigger a Major Nonconformity during an FSSC 22000 audit. First, relying on ATP luminometers instead of protein-specific ELISA / LFD swabs after allergen changeovers. Second, collecting EMP swabs immediately after pre-shift disinfection rather than 3-4 hours into active production when equipment vibration shakes hidden biofilms loose from bearings and seals. Third, citing withdrawn specifications (ISO/TS 22002-1:2009 or PAS 223) in active food safety manuals.
| Yaremche Practicum Engineering Module | Normative Reference (ISO 22002:2025 + FSSC 22000) | Quantitative Target Metric | Shop-Floor and Laboratory Verification Tool | Audit Evidence Package Required by Certification Body |
|---|---|---|---|---|
| HVAC Positive Pressure Cascade and Air Filtration in High Care Zones | ISO 22002-100:2025 (Clauses 5-6) + ISO 22002-1:2025 | Pressure differential Delta P = 5-15 Pa; F7-F9 + HEPA H13 filtration; zero ceiling condensate | Differential pressure gauges, thermo-hygrometers, settle plates or active volumetric air samplers | Daily Delta P logs, filter replacement records triggered by pressure drop, microbiological air test reports |
| Hydrodynamic and Chemical Validation of Closed-Loop CIP | ISO 22002-100:2025 (Clause 10) + ISO 22002-1:2025 + FSSC 2.5.12 | Flow velocity v >= 1.5 m/s (Re > 25,000); NaOH 1.5-2.2% (68-75 °C); dead legs L/D < 1.5 | Electromagnetic flowmeter, CIP Return conductivity probe, 365 nm UV lamp (riboflavin), lab titration | Annual CIP validation report, SCADA cycle charts, final rinse pH/conductivity and microbiological swab logs |
| Allergen Changeover Sanitation Validation and Release | ISO 22002-100:2025 (Clause 12) + ISO 22002-1:2025 + FSSC 2.5.6 | Target allergen protein residue below limit of quantification (< 1-5 ppm on Zone 1 surfaces) | Allergen-specific LFD rapid strips on shop floor + quantitative ELISA in ISO/IEC 17025 accredited lab | Line allergen matrix, 3-run consecutive validation dossier, photographic disassembly guides for operators |
| Environmental Monitoring Program for Pathogens (EMP Zones 1-4) | ISO 22002-1:2025 + FSSC 22000 Additional Requirement 2.5.7 | Absence of Listeria monocytogenes and Salmonella spp. per 25 g / 100 cm2 swabbed area | Neutralizing buffer sponges (Dey-Engley / Letheen broth), testing per ISO 11290 and ISO 6579 | Scaled Zone 1-4 plant map, quarterly pathogen trend heatmaps, Seek and Destroy root-cause investigation logs |
| Packaging Chemical Migration and NIAS Control (Category I) | ISO 22002-100:2025 + ISO 22002-4:2025 + FSSC 2.5.4 | Overall migration OML <= 10 mg/dm2 (or <= 60 mg/kg); specific migration SML within legal limits | Gas and liquid chromatography-mass spectrometry (GC-MS / LC-MS) in food simulants A, B, C, D1, D2 | Supplier Declaration of Compliance (DoC) backed by accredited ISO/IEC 17025 lab reports and low-migration ink certificates |
| Food Defense (TACCP) and Food Fraud Vulnerability Control (VACCP) | ISO 22002-100:2025 (Clause 18) + FSSC 22000 Additional Requirements 2.5.3 and 2.5.4 | 100% physical access control on bulk intakes; mass-balance reconciliation within 98.5-100.5% | Physical intrusion drills, tamper-evident seal audits, isotope or DNA authenticity testing on vulnerable inputs | TACCP threat and VACCP vulnerability matrices, annual intrusion drill reports, batch mass-balance sheets |
FSSC 22000 Audit Simulation: ISO 22000 Change Management, 4-Hour Traceability Drills, and Laboratory Verification
Another practical session in Yaremche connected the new ISO 22002-100:2025 clauses directly to management system requirements in ISO 22000 (Clauses 6.3, 7.1.6, 8.2, 8.3, and 8.5). During a real FSSC 22000 certification or surveillance audit, an auditor never looks at prerequisite programs in isolation. They test how your PRPs interact with Management of Change (MoC), vertical and horizontal traceability drills, and accredited laboratory verification.
Engineering Change Management Under Clause 6.3 of ISO 22000
We walked teams through a scenario that happens on factory floors every month: during a night-shift breakdown, a maintenance technician replaces a homogenizer seal or welds a new dosing nozzle onto a mixing tank without notifying the Food Safety Team. Production resumes at dawn, but the new pipe branch creates a dead leg ($L/D = 3.2$) that routine CIP flow can't reach. Under ISO 22002-100:2025 (Clause 9) and Clause 6.3 of ISO 22000, any equipment modification, sanitation chemical switch, packaging film substitution, or room layout adjustment requires a documented risk assessment prior to commissioning.
Participants in Yaremche built a one-page Management of Change (MoC) Gate Form requiring sign-off across three disciplines:
- Hygienic Engineering Check: confirming stainless steel grade (
AISI 316Lfor acidic or salty products), internal weld surface roughness ($R_a \le 0.8\text{ }\mu\text{m}$), and valid Food Contact Material (FCM) certificates for all gaskets (EPDM,PTFE, food-grade silicone); - HACCP and PRP Matrix Review: evaluating whether the engineering change introduces new physical, chemical, allergenic, or microbiological hazards under Clause 8.5 of ISO 22000;
- Sanitation Re-Validation and Operator Briefing: running three consecutive cleaning and swabbing cycles before releasing the modified line for commercial production.
Running the 4-Hour Bidirectional Traceability and Mass-Balance Stress Test
Under Clause 16 of ISO 22002-100:2025 and GFSI benchmarking rules, certified sites must complete a full forward and backward traceability exercise, including a quantitative mass-balance reconciliation, within a strict audit window (typically under 4 hours). In Yaremche, we ran a timed simulation where each team drew a random finished-product batch code and mapped every linked record.
While every team could trace bulk ingredients (flour, raw milk, meat cuts), our stress test exposed gaps in four secondary streams now scrutinized under ISO 22002-100:2025 and its sector parts (-1, -4, -5):
- Primary Packaging and Process Gases: linking the finished batch to the exact lot number of flexible film, hot-melt adhesive, or food-grade modified atmosphere gas (
CO2 / N2) used on that shift. - Internal Rework Loops (
Rework): accounting for the exact percentage, original production date, and allergen profile of semi-finished rework blended back into the batch. - Sanitation Chemical Lot Traceability: proving which batch of peracetic acid or caustic detergent sanitized the holding tank prior to filling, alongside the operator's zero-residue rinse verification signature.
- Cold-Chain Transport History (
ISO 22002-5:2025): tying each dispatched pallet to the specific reefer trailer, multi-point temperature logger graph, and pre-loading washout certificate.
Verifying Testing Laboratories Under ISO/IEC 17025 and NAAU Scope Registries
We also audited how enterprises verify external laboratory data. Under FSSC 22000 Additional Requirement 2.5.1(e), all analyses that verify food safety controls (PRP, OPRP, CCP, EMP pathogen swabs, potable water, packaging migration, pesticide residues, mycotoxins, and veterinary drugs) must be performed by testing laboratories accredited to ISO/IEC 17025 or participating in recognized proficiency testing schemes. During the workshop, teams looked up their contracted laboratories in the official registry of the National Accreditation Agency of Ukraine (NAAU) and caught cases where a lab held a general ISO/IEC 17025 certificate, but the specific test method for Listeria monocytogenes or phthalate migration wasn't listed inside its accredited scope annex.
Team Workshop Methodology in Yaremche: Cross-Functional Audit Simulations and Resolving Shop-Floor Conflicts
Why did an offsite workshop in the Carpathians generate faster operational change than standard classroom training? We refused to work from generic templates and instead structured every exercise around the real cross-functional friction that plays out daily between quality assurance, production management, maintenance engineering, and procurement.
Role-Playing Real Conflicts Between Production Uptime and Sanitation
Every food plant faces the same tension: the production manager is measured on shift output and Overall Equipment Effectiveness (OEE), while the Food Safety Team leader demands a 90-minute line shutdown to dismantle a depositor, run a full caustic wash, and swab for peanut protein before switching to an allergen-free batch. Inside the factory, that argument often ends in a rushed wash or a rubber-stamped logbook.
In Yaremche, we seated production supervisors, chief mechanics, procurement specialists, and QA managers at the same table and swapped their roles in simulated FSSC 22000 audits. When a production manager plays the lead auditor and sees firsthand how an unwashed homogenizer dead leg or a torn sifter mesh triggers certificate suspension and halts retail exports, resistance to PRP discipline vanishes. That shared ownership is the foundation of Food Safety Culture required by both GFSI and ISO 22002-100:2025.
Open Engineering Exchange Across Food, Packaging, and Logistics Sectors
The atmosphere in Yaremche was focused, candid, and genuinely enjoyable. Between technical blocks, specialists from dairy plants, meat processors, industrial bakeries, flexible packaging converters, and cold-chain carriers compared practical fixes: which foam stations hold pressure longest, how to rodent-proof loading docks during autumn harvest, and how to structure sampling calendars. Teams didn't just listen to lectures; they tested engineering fixes against their own plant constraints and left with a synchronized action plan.
Photo Report from Ekontrol's Offsite Engineering Practicum in Yaremche
Below is our photo report capturing the working groups, engineering case defenses, ISO 22002-100:2025 matrix reviews, and team discussions during Ekontrol's offsite training practicum in Yaremche on January 28, 2025.
From Training to Certification: Corporate Workshops, Pre-Audit Diagnostics, and 90-Day Implementation with Ekontrol
Training a Food Safety Team delivers real return on investment when workshop decisions turn into measurable engineering and procedural upgrades on the plant floor. Every team leaving our Yaremche practicum returned to their facility with a structured 90-day transition roadmap for ISO 22002:2025 and updated compliance protocols for FSSC 22000, ISO 22000, and HACCP.
The 90-Day Post-Training Engineering Transition Roadmap
Experience across Ekontrol industrial projects shows that asking a single quality manager to rewrite all PRP procedures in a week produces paper-only compliance that collapses during an unannounced audit. Instead, sustainable readiness follows a four-stage engineering cycle:
- Days 1-20: Pre-Training or Post-Training Shop-Floor Diagnostic Audit. Our lead auditors walk your entire production flow alongside your FST, inspecting hygienic zoning,
HVACpressure cascades,CIPreturn loops, floor drains, chemical stores, and packaging warehouses againstISO 22002-100:2025and your sector standard (-1,-4,-5). - Days 21-45: Tailored Corporate Practicum and Documentation Re-Engineering Under Management System Implementation. We run a site-specific workshop built around your exact equipment, eliminate duplicated
PRPinstructions, update your hazard analysis under Clause 8.5 of ISO 22000, and formalize change management under Clause 6.3. - Days 46-75: Instrumental and Accredited Laboratory Validation. Together with your chief engineer and laboratory staff, we validate
CIPcleaning regimes, verify allergen changeover protocols, mapEMPswabbing points across Zones 1-4, and test packaging migration in accredited testing laboratories compliant with ISO/IEC 17025. - Days 76-90: Unannounced Mock Audit, Certification Audit Support, and Ongoing Annual System Support. We conduct a full-scale unannounced stress audit, close root causes using
CAPAmethodology, coach line operators for auditor interviews, and back your team during certification body assessments.
If your facility is preparing for the ISO 22002-100:2025 transition, facing an upcoming FSSC 22000 surveillance or recertification audit, or needs a hands-on offsite or on-site engineering workshop for your Food Safety Team, reach out to Ekontrol specialists via our contact page.
| Ekontrol Corporate Preparation Stage | Implementation Timeline | Plant Team Participants | Engineering and Methodological Scope | Deliverable for Management and Certification Auditors |
|---|---|---|---|---|
| Stage 1. On-Site Pre-Audit Gap Analysis (/diagnostic-audit) | Weeks 1-3 (Days 1-20) | Quality Director, FST Leader, Chief Engineer, Production Manager | Physical inspection of hygienic zoning, HVAC, CIP, drainage, storage, and lab controls against ISO 22002-100:2025 and sector parts (-1, -4, -5) | Photographic gap report, risk heatmap, and prioritized CAPEX/OPEX engineering remediation plan |
| Stage 2. Customized Offsite or On-Site FST Engineering Practicum | Weeks 4-5 (Days 21-35) | Full Food Safety Team, shift supervisors, technologists, procurement leads, internal auditors | Hands-on workshop using your plant blueprints: cross-contamination mapping, allergen validation, EMP Zones 1-4, TACCP and VACCP drills | Trained cross-functional team with personal certificates and agreed dual-standard PRP procedure templates |
| Stage 3. PRP Overhaul and Lab Validation (/implementation and /iso-17025) | Weeks 6-10 (Days 36-75) | FST working group, plant laboratory, mechanical and utilities engineering department | Migration to two-tier SOP architecture, CIP and allergen cleaning validation, EMP and packaging migration testing in ISO/IEC 17025 labs | Updated FSSC 22000 / ISO 22000 documentation suite and complete validation dossier for critical processes |
| Stage 4. Mock Stress Audit, Certification Defense, and Maintenance (/audit-support and /annual-support) | Weeks 11-13 (Days 76-90) and ongoing | Plant leadership, shop-floor operators, Food Safety Team | Unannounced mock FSSC 22000 audit, operator interview coaching, CAPA closure verification, and quarterly surveillance support | Successful certification or surveillance audit with zero critical or major nonconformities and stable compliance |
Measurable Plant Impact from Combining FST Practicums with Ekontrol Diagnostic Audits
Across Ekontrol industrial projects in 2025-2026, manufacturing sites that paired a hands-on FST engineering workshop with a pre-audit shop-floor diagnostic under ISO 22002-100:2025 and its sector standards cut allergen line-changeover downtime by 18-25% and reduced minor nonconformities during FSSC 22000 certification audits by threefold on average.
Book a Custom ISO 22002-100:2025 Corporate Workshop or FSSC 22000 Diagnostic Audit
Ekontrol lead auditors and engineers will tailor a practical training program to your plant processes, run a shop-floor PRP gap analysis, and prepare your Food Safety Team for certification audits.
Request a training or audit proposal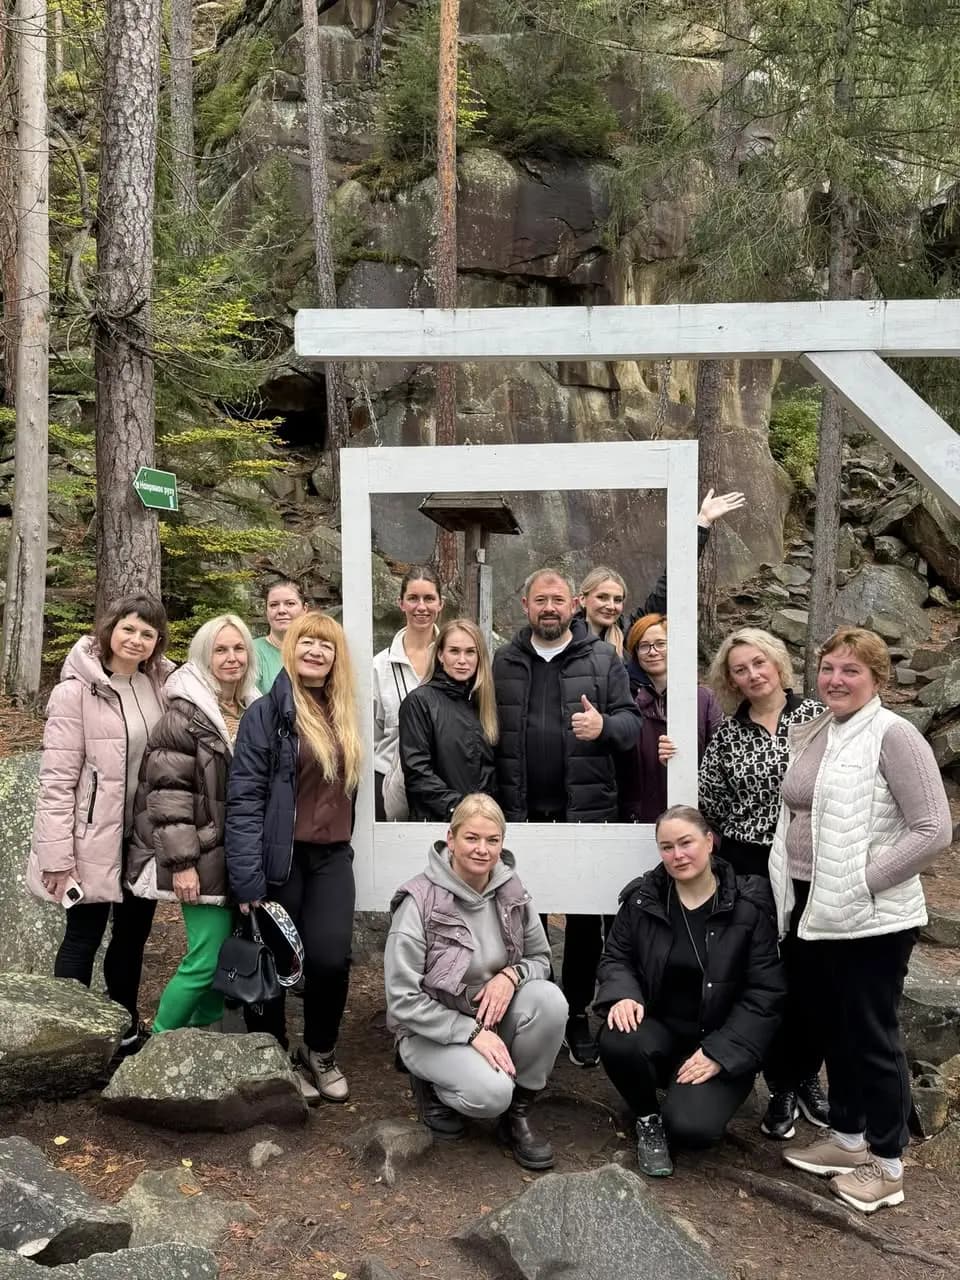
Need a certification consultation?
Free ConsultationOn This Page
- Ekontrol Engineering Practicum in Yaremche: ISO 22002-100:2025 and FSSC 22000 Workshop Outcomes for FSTs
- Two-Tier Architecture of ISO 22002-100:2025 and Sector Standards (-1, -4, -5): Practical Breakdown
- Shop-Floor Case Studies (Category C): Hygienic Zoning, HVAC Positive Pressure, and CIP Validation Under ISO 22002-1:2025
- Packaging Migration (ISO 22002-4:2025), Allergen Swabbing, EMP Zoning (Zones 1-4), and TACCP/VACCP Defense
- FSSC 22000 Audit Simulation: ISO 22000 Change Management, 4-Hour Traceability Drills, and Laboratory Verification
- Team Workshop Methodology in Yaremche: Cross-Functional Audit Simulations and Resolving Shop-Floor Conflicts
- Photo Report from Ekontrol's Offsite Engineering Practicum in Yaremche
- From Training to Certification: Corporate Workshops, Pre-Audit Diagnostics, and 90-Day Implementation with Ekontrol
- Frequently Asked Questions About Ekontrol Corporate Training, ISO 22002-100:2025 Transition, and FSSC 22000 Audits
Ekontrol Engineering Practicum in Yaremche: ISO 22002-100:2025 and FSSC 22000 Workshop Outcomes for FSTs
On January 28, 2025, the Ekontrol lead auditor and engineering team hosted an intensive offsite practicum in Yaremche dedicated to the structural overhaul of the ISO 22002:2025 series and its direct impact on FSSC 22000 certification audits. Rather than running a slide-based lecture, we built the event as a hands-on engineering workshop for active Food Safety Teams (FSTs): quality directors, chief technologists, chief engineers, sanitation managers, laboratory heads, and internal auditors from food processing, packaging, feed, and cold-chain logistics enterprises.
Why did this structural reform require an immediate engineering response? Technical committee ISO/TC 34/SC 17 replaced the standalone technical specifications ISO/TS 22002-1:2009, ISO/TS 22002-2:2013, ISO/TS 22002-4:2013, ISO/TS 22002-5:2019, and ISO/TS 22002-6:2016 with full international standards anchored by the umbrella standard ISO 22002-100:2025. Most manufacturing sites still operate with prerequisite programs (PRPs) drafted around legacy ISO 22002-1:2005 or ISO/TS 22002-1:2009 clauses. Those older documents don't match the new two-tier structure or the latest benchmarking criteria enforced by the Global Food Safety Initiative (GFSI).
Why Standard Classroom Lectures Fail Food Safety Teams
When a quality manager attends a routine webinar from their desk at the plant, operational emergencies interrupt them every twenty minutes. A raw material truck arrives with a broken seal, a filler line stops for unplanned sanitation, or a buyer requests an urgent specification update. Training notes end up in a drawer while shop-floor PRP procedures remain untouched for months. Pulling multidisciplinary teams out of daily plant firefighting to Yaremche solved that problem.
Before arriving at the workshop, participating teams assembled real technical dossiers from their facilities: master PRP matrices, architectural zoning blueprints, air handling (HVAC) schematics, Clean-in-Place (CIP) validation logs, Environmental Monitoring Program (EMP) swabbing maps, and nonconformity reports from recent surveillance audits. Over the course of the session, each team ran a clause-by-clause gap analysis of their own documentation, exposed blind spots between maintenance and quality departments, and built a practical schedule for upgrading their ISO 22000 food safety management system.
Honestly, the biggest realization for many participants was that the highest risks during the ISO 22002-100:2025 transition sit in physical plant utilities and missing metrological proof, not in document numbering. When a chief engineer and an FST leader examine floor drain gradients or air pressure differentials across a high-care packaging wall together, years of departmental friction disappear in minutes.
The Dual-Standard Audit Rule Practiced During the Yaremche Workshop
During the Yaremche practicum, participating teams practiced the core regulatory rule of the 2025 architecture: the umbrella standard ISO 22002-100:2025 cannot be used on its own. During an FSSC 22000 certification audit, the auditor verifies an inseparable pair of standards: all 18 common clauses of ISO 22002-100:2025 combined with your sector-specific standard (ISO 22002-1:2025 for Category C, ISO 22002-4:2025 for Category I, or ISO 22002-5:2025 for Category G). If your PRP matrix doesn't cross-reference both tiers, certification bodies record a systemic nonconformity under Clause 8.2 of ISO 22000.
Two-Tier Architecture of ISO 22002-100:2025 and Sector Standards (-1, -4, -5): Practical Breakdown
The opening module of the Yaremche training unpacked the structural shift from legacy specifications (ISO 22002-1:2005 / PAS 220 / ISO/TS 22002-1:2009) to the two-tier ISO 22002:2025 series. Under the old system, every link in the food supply chain had a separate specification where 75-80% of the text repeated identical baseline rules for building layout, pest control, personal hygiene, waste handling, and chemical storage. Meanwhile, wording differences across those separate documents created headaches for multi-site groups regarding allergen control, cross-contamination, and supplier approval.
In the new architecture, all universal prerequisite requirements sit inside the common umbrella standard ISO 22002-100:2025, harmonized with the General Principles of Food Hygiene of Codex Alimentarius (CXC 1-1969, 2020/2022 revision). The sector parts (ISO 22002-1:2025, ISO 22002-2:2025, ISO 22002-4:2025, ISO 22002-5:2025, ISO 22002-6:2025, and ISO 22002-7:2025) now contain only process-specific engineering controls for each respective supply chain category.
How Teams Restructured PRP Documentation Without Paper Bloat
We split participants into working groups by industry category and gave them a concrete engineering assignment: migrate existing PRP manuals to the dual-standard format without creating dozens of redundant standard operating procedures (SOPs). Teams worked through six practical tasks:
- SOP De-duplication Across Multi-Site Operations: consolidating the 18 universal clauses of
ISO 22002-100:2025into a single corporate baseline manual for vertically integrated groups operating processing plants, warehouses, and transport fleets. - Sector Add-Ons Under
ISO 22002-1:2025(Category C): specifying hygienic equipment design, sanitation validation, foreign body prevention (metal detectors, X-ray inspection, sifters, neodymium magnetic traps with induction $\ge 10,000\text{ Gauss}$), and rework segregation. - Food Packaging Controls Under
ISO 22002-4:2025(Category I): replacing legacyISO/TS 22002-4:2013references with strict verification of chemical migration, printing inks, photoinitiators, adhesives, and residual solvents. - Transport and Cold-Storage Controls Under
ISO 22002-5:2025(Category G): defining 3D thermal mapping for warehouses and reefers, dock-door discipline, cross-docking hygiene, and tanker washout verification. - Integration With ISO 22000 and HACCP Hazard Analysis: drawing a sharp boundary between baseline
PRPs, operational prerequisite programs (OPRPs), and critical control points (CCPs) under the official FSSC 22000 scheme. - Unannounced Audit Evidence Design: building shift verification checklists that operators can complete in three minutes while generating an indisputable audit trail.
The engineering table below summarizes the cross-sector mapping matrix compiled by teams during the Yaremche practicum.
| Supply Chain Sector and FSSC 22000 Category | Legacy Specification (Pre-2025) | New Paired Architecture (ISO 22002:2025) | Yaremche Workshop Case Focus | Typical Audit Gap Identified by Participating Teams |
|---|---|---|---|---|
| Food Manufacturing (Category C: C0, CI, CII, CIII, CIV) | ISO 22002-1:2005 (early editions) and ISO/TS 22002-1:2009 | ISO 22002-100:2025 + ISO 22002-1:2025 | Hygienic zoning, HVAC pressure cascades, CIP validation, allergen changeover, floor drainage direction | No instrumental differential pressure logs between zones and visual-only sign-off after line sanitation |
| Food Packaging and Container Manufacturing (Category I) | PAS 223:2011 and ISO/TS 22002-4:2013 | ISO 22002-100:2025 + ISO 22002-4:2025 | Overall (OML) and specific (SML) migration testing, NIAS screening, functional barriers, ink set-off in reels | Supplier Declarations of Compliance lack ISO/IEC 17025 lab test reports in appropriate food simulants |
| Transport, Cold Chain, and Storage Logistics (Category G) | ISO/TS 22002-5:2019 | ISO 22002-100:2025 + ISO 22002-5:2025 | 3D reefer thermal mapping, cross-docking temperature recovery, EFTCO tanker cleaning certificates, load security | Temperature data loggers mounted only near evaporator outlets without monitoring the warmest spot near rear doors |
| Animal Feed and Premix Manufacturing (Category D) | PAS 222:2011 and ISO/TS 22002-6:2016 | ISO 22002-100:2025 + ISO 22002-6:2025 | Mixer homogeneity validation (CV <= 5%), medicated feed carry-over prevention, sequencing and flushing | Flushing batches used between medicated and non-medicated runs without quantitative lab verification of active residue |
| Catering, Food Service, Retail, and Wholesale (Categories E, F) | ISO/TS 22002-2:2013 and local hygiene codes | ISO 22002-100:2025 + ISO 22002-2:2025 / ISO 22002-7:2025 | Blast-chilling kinetics (+60 °C to +10 °C <= 2 hours), display cabinet cold chain, FEFO stock rotation | Manual temperature checks recorded twice per shift with no automated alarm logging during peak defrost cycles |
Shop-Floor Case Studies (Category C): Hygienic Zoning, HVAC Positive Pressure, and CIP Validation Under ISO 22002-1:2025
The most intense technical debates during the Yaremche group sessions centered on ISO 22002-100:2025 and ISO 22002-1:2025 requirements for food processing facilities (dairies, meat processing plants, bakeries, confectionery lines, and beverage bottlers). Each group had to defend a real plant layout and sanitation protocol in front of an audit panel made up of Ekontrol lead auditors and engineers from peer companies.
Case 1: Hygienic Zoning, Traffic Segregation, and HVAC Positive Pressure Cascades
When reviewing an actual floor plan for a Ready-to-Eat (RTE) dairy packaging hall, participants spotted a classic architectural flaw: pallets of outer corrugated cardboard crossed the same corridor used by operators entering the High Care / High Hygiene zone after changing boots and coveralls. Under older practices, the plant tried to manage that hazard through time separation on a schedule. However, ISO 22002-100:2025 (Clause 5) and ISO 22002-1:2025 demand physical barrier segregation and complete elimination of intersecting paths between raw materials, finished exposed products, waste, and outer packaging.
Working alongside plant engineers, teams calculated the aerodynamic barrier required from the heating, ventilation, and air conditioning (HVAC) system. Preventing unfiltered air from being sucked from medium-hygiene or ambient corridors into open-product filling rooms requires a continuous positive static pressure differential:
$$\Delta P = P_{\text{high care}} - P_{\text{medium hygiene}} \ge 5\text{-}15\text{ Pa}$$
During the workshop, teams drafted concrete engineering specifications for their maintenance departments:
- installing Magnehelic differential pressure gauges (or digital pressure transmitters linked to SCADA) directly at airlock doors between zones with visual alarms if doors stay propped open;
- equipping clean-zone air handling units with multi-stage filtration rated at
F7-F9(ISO 16890ePM1 55-80%) and terminalHEPA H13/H14filters (EN 1822), replacing filter cassettes based on maximum pressure-drop thresholds rather than arbitrary six-month calendar dates; - controlling indoor dew-point temperature ($T_{\text{dew}}$) in chilled processing rooms so condensation never forms on ceiling panels, overhead ducts, or evaporator fins, eliminating a primary vector for Listeria monocytogenes droplets;
- configuring floor drainage channels with trapped gullies and backflow preventers so effluent flows strictly from
High CaretowardBasic Hygieneareas at a floor slope of1.5-2.0%without standing puddles.
Case 2: Engineering Validation of Clean-in-Place (CIP) Circuits Using Sinner's Circle
Our second shop-floor case examined closed-circuit CIP sanitation records. Across FSSC 22000 audits, more than 40% of sanitation nonconformities happen because Food Safety Teams confuse daily operational monitoring with initial engineering validation and periodic verification. In Yaremche, teams applied Sinner's Circle parameters (fluid mechanics, thermal energy, chemical concentration, contact time) to their own CIP logs and uncovered three frequent engineering failures:
- Velocity Drop in Stepped-Diameter Piping: if a centrifugal pump drives caustic wash liquid through a
DN 50pipe at $v = 1.8\text{ m/s}$, expanding that same flow into aDN 80manifold drops linear velocity inversely with the square of pipe diameter down to $v \approx 0.7\text{ m/s}$. At that speed, the Reynolds number ($Re = \frac{v \cdot D}{\nu}$) falls below the turbulent scrubbing threshold ($Re < 25,000$), leaving boundary-layer biofilm intact regardless of caustic temperature. - Measuring Dosing Pump Strokes Instead of Return-Line Conductivity (
CIP Return): caustic soda (NaOHat1.5-2.2%and68-75 °C) and nitric or phosphoric acid (HNO3at0.8-1.2%and55-65 °C) must be controlled via temperature-compensated conductivity sensors mounted on theCIP Returnline, backed up by manual acid-base titration in the plant laboratory. - Dead Legs and Spray-Ball Shadow Zones: under
EHEDGhygienic design rules, any T-piece or instrument branch must maintain a length-to-diameter ratio of $L/D < 1.5$ (and never above $2.0$). Participants practiced documenting riboflavin fluorescence spray tests under365 nmUV light to verify 100% wetting of tank domes, agitator shafts, and manway gaskets during equipment commissioning.
Packaging Migration (ISO 22002-4:2025), Allergen Swabbing, EMP Zoning (Zones 1-4), and TACCP/VACCP Defense
A dedicated engineering module at the Yaremche practicum addressed sector requirements for packaging manufacturers (ISO 22002-4:2025) and logistics operators (ISO 22002-5:2025), alongside cross-cutting FSSC 22000 additional requirements: allergen changeover validation, Environmental Monitoring Programs (EMP), Food Defense (TACCP), and Food Fraud mitigation (VACCP).
Case 3: Packaging Migration, NIAS, and Printing Ink Set-Off Under ISO 22002-4:2025
Working with packaging converters and food-plant procurement specialists, we examined how ISO 22002-4:2025 tightens controls over primary food contact materials (flexible multilayer films, PET preforms, paperboard trays, and metal cans). Participants audited real Declarations of Compliance (DoC) from their current packaging suppliers and discovered that 65% of the files lacked migration test reports performed in the correct food simulants (Simulants A, B, C, D1, and D2 under EU Regulation 10/2011).
During the group exercise, teams built a technical verification protocol covering four mandatory parameters:
- verifying the Overall Migration Limit (
OML$\le 10\text{ mg/dm}^2$ of contact surface or $\le 60\text{ mg/kg}$ of food simulant) and Specific Migration Limits (SML) for monomers, plasticizers, antioxidants, and catalysts; - screening Non-Intentionally Added Substances (
NIAS), including polymer thermal degradation byproducts formed during high-temperature extrusion, oligomers, and contaminants in recycled polymers (rPET); - preventing invisible
set-offtransfer of low-molecular-weight UV ink photoinitiators and coatings from the printed outer surface onto the food-contact inner surface when flexible film is wound under high tension on slitter-rewinders; - running gas chromatography headspace tests for residual lamination solvents (ethyl acetate, methoxypropanol, isopropanol) in testing laboratories accredited to ISO/IEC 17025.
Case 4: Allergen Changeover Validation and the ATP Bioluminescence Misconception
In the allergen management workshop (updated Clause 12 of ISO 22002-100:2025, expanded in ISO 22002-1:2025 and FSSC 22000 Additional Requirement 2.5.6), we tackled a widespread misconception that trips up nearly half of food plants during certification audits. Several teams assumed that an ATP bioluminescence swab reading below 10-30 RLU after wet or dry line cleaning proved the absence of allergens such as milk casein, gluten, soy, peanut, hazelnut, or egg protein.
In Yaremche, we demonstrated why auditors reject that practice: ATP luminometers detect adenosine triphosphate from living or recently lysed cells and general organic soil, whereas allergenic proteins don't contain ATP and remain immunochemically active even after baking, roasting, or pasteurization. Validating a changeover from an allergen-containing recipe to a free-from product requires allergen-specific Lateral Flow Devices (LFDs with 1-5 ppm detection thresholds) for routine shift release and quantitative ELISA immunoassays across three consecutive production cleanings for formal method validation.
Case 5: Environmental Monitoring Program Zoning (EMP Zones 1-4) and TACCP/VACCP Drills
Next, teams mapped pathogen swabbing points onto their plant drawings under FSSC 22000 Additional Requirement 2.5.7 and ISO 22002-1:2025, dividing facilities into four concentric hygienic zones:
- Zone 1 (Direct Food Contact Surfaces post-lethality): slicer blades, depositor nozzles, conveyor belts, filling hoppers, and packaging chutes.
- Zone 2 (Adjacent Non-Food Contact Surfaces): equipment frames, operator touchscreens, drip pans underneath overhead evaporators, and exterior filler housings.
- Zone 3 (Remote Processing Room Surfaces): floor drains, P-traps, pallet-jack wheels, walls, door handles, and squeegees.
- Zone 4 (Areas Outside the Processing Room): locker rooms, maintenance workshops, raw-material warehouses, and corridors.
Teams drafted a Seek and Destroy escalation protocol whenever Listeria spp. or Salmonella spp. turns up in Zone 2 or Zone 3: vector swabbing within a 2-3 meter radius around the positive point, disassembling hollow rollers and gaskets to locate harborage niches, and executing deep chemical-thermal sanitation before the pathogen reaches Zone 1.
In parallel, during the TACCP (Food Defense) and VACCP (Food Fraud) tabletop exercise, participants tested physical security locks on outdoor bulk silos, CIP chemical cabinets, and water storage tanks, while writing mass-balance equations to catch economically motivated adulteration in high-risk ingredients (cocoa butter, olive oil, milk powder, spices).
Three High-Risk Audit Findings Teams Uncovered in Their Own Procedures
Reviewing actual plant procedures in Yaremche exposed three systemic vulnerabilities that trigger a Major Nonconformity during an FSSC 22000 audit. First, relying on ATP luminometers instead of protein-specific ELISA / LFD swabs after allergen changeovers. Second, collecting EMP swabs immediately after pre-shift disinfection rather than 3-4 hours into active production when equipment vibration shakes hidden biofilms loose from bearings and seals. Third, citing withdrawn specifications (ISO/TS 22002-1:2009 or PAS 223) in active food safety manuals.
| Yaremche Practicum Engineering Module | Normative Reference (ISO 22002:2025 + FSSC 22000) | Quantitative Target Metric | Shop-Floor and Laboratory Verification Tool | Audit Evidence Package Required by Certification Body |
|---|---|---|---|---|
| HVAC Positive Pressure Cascade and Air Filtration in High Care Zones | ISO 22002-100:2025 (Clauses 5-6) + ISO 22002-1:2025 | Pressure differential Delta P = 5-15 Pa; F7-F9 + HEPA H13 filtration; zero ceiling condensate | Differential pressure gauges, thermo-hygrometers, settle plates or active volumetric air samplers | Daily Delta P logs, filter replacement records triggered by pressure drop, microbiological air test reports |
| Hydrodynamic and Chemical Validation of Closed-Loop CIP | ISO 22002-100:2025 (Clause 10) + ISO 22002-1:2025 + FSSC 2.5.12 | Flow velocity v >= 1.5 m/s (Re > 25,000); NaOH 1.5-2.2% (68-75 °C); dead legs L/D < 1.5 | Electromagnetic flowmeter, CIP Return conductivity probe, 365 nm UV lamp (riboflavin), lab titration | Annual CIP validation report, SCADA cycle charts, final rinse pH/conductivity and microbiological swab logs |
| Allergen Changeover Sanitation Validation and Release | ISO 22002-100:2025 (Clause 12) + ISO 22002-1:2025 + FSSC 2.5.6 | Target allergen protein residue below limit of quantification (< 1-5 ppm on Zone 1 surfaces) | Allergen-specific LFD rapid strips on shop floor + quantitative ELISA in ISO/IEC 17025 accredited lab | Line allergen matrix, 3-run consecutive validation dossier, photographic disassembly guides for operators |
| Environmental Monitoring Program for Pathogens (EMP Zones 1-4) | ISO 22002-1:2025 + FSSC 22000 Additional Requirement 2.5.7 | Absence of Listeria monocytogenes and Salmonella spp. per 25 g / 100 cm2 swabbed area | Neutralizing buffer sponges (Dey-Engley / Letheen broth), testing per ISO 11290 and ISO 6579 | Scaled Zone 1-4 plant map, quarterly pathogen trend heatmaps, Seek and Destroy root-cause investigation logs |
| Packaging Chemical Migration and NIAS Control (Category I) | ISO 22002-100:2025 + ISO 22002-4:2025 + FSSC 2.5.4 | Overall migration OML <= 10 mg/dm2 (or <= 60 mg/kg); specific migration SML within legal limits | Gas and liquid chromatography-mass spectrometry (GC-MS / LC-MS) in food simulants A, B, C, D1, D2 | Supplier Declaration of Compliance (DoC) backed by accredited ISO/IEC 17025 lab reports and low-migration ink certificates |
| Food Defense (TACCP) and Food Fraud Vulnerability Control (VACCP) | ISO 22002-100:2025 (Clause 18) + FSSC 22000 Additional Requirements 2.5.3 and 2.5.4 | 100% physical access control on bulk intakes; mass-balance reconciliation within 98.5-100.5% | Physical intrusion drills, tamper-evident seal audits, isotope or DNA authenticity testing on vulnerable inputs | TACCP threat and VACCP vulnerability matrices, annual intrusion drill reports, batch mass-balance sheets |
FSSC 22000 Audit Simulation: ISO 22000 Change Management, 4-Hour Traceability Drills, and Laboratory Verification
Another practical session in Yaremche connected the new ISO 22002-100:2025 clauses directly to management system requirements in ISO 22000 (Clauses 6.3, 7.1.6, 8.2, 8.3, and 8.5). During a real FSSC 22000 certification or surveillance audit, an auditor never looks at prerequisite programs in isolation. They test how your PRPs interact with Management of Change (MoC), vertical and horizontal traceability drills, and accredited laboratory verification.
Engineering Change Management Under Clause 6.3 of ISO 22000
We walked teams through a scenario that happens on factory floors every month: during a night-shift breakdown, a maintenance technician replaces a homogenizer seal or welds a new dosing nozzle onto a mixing tank without notifying the Food Safety Team. Production resumes at dawn, but the new pipe branch creates a dead leg ($L/D = 3.2$) that routine CIP flow can't reach. Under ISO 22002-100:2025 (Clause 9) and Clause 6.3 of ISO 22000, any equipment modification, sanitation chemical switch, packaging film substitution, or room layout adjustment requires a documented risk assessment prior to commissioning.
Participants in Yaremche built a one-page Management of Change (MoC) Gate Form requiring sign-off across three disciplines:
- Hygienic Engineering Check: confirming stainless steel grade (
AISI 316Lfor acidic or salty products), internal weld surface roughness ($R_a \le 0.8\text{ }\mu\text{m}$), and valid Food Contact Material (FCM) certificates for all gaskets (EPDM,PTFE, food-grade silicone); - HACCP and PRP Matrix Review: evaluating whether the engineering change introduces new physical, chemical, allergenic, or microbiological hazards under Clause 8.5 of ISO 22000;
- Sanitation Re-Validation and Operator Briefing: running three consecutive cleaning and swabbing cycles before releasing the modified line for commercial production.
Running the 4-Hour Bidirectional Traceability and Mass-Balance Stress Test
Under Clause 16 of ISO 22002-100:2025 and GFSI benchmarking rules, certified sites must complete a full forward and backward traceability exercise, including a quantitative mass-balance reconciliation, within a strict audit window (typically under 4 hours). In Yaremche, we ran a timed simulation where each team drew a random finished-product batch code and mapped every linked record.
While every team could trace bulk ingredients (flour, raw milk, meat cuts), our stress test exposed gaps in four secondary streams now scrutinized under ISO 22002-100:2025 and its sector parts (-1, -4, -5):
- Primary Packaging and Process Gases: linking the finished batch to the exact lot number of flexible film, hot-melt adhesive, or food-grade modified atmosphere gas (
CO2 / N2) used on that shift. - Internal Rework Loops (
Rework): accounting for the exact percentage, original production date, and allergen profile of semi-finished rework blended back into the batch. - Sanitation Chemical Lot Traceability: proving which batch of peracetic acid or caustic detergent sanitized the holding tank prior to filling, alongside the operator's zero-residue rinse verification signature.
- Cold-Chain Transport History (
ISO 22002-5:2025): tying each dispatched pallet to the specific reefer trailer, multi-point temperature logger graph, and pre-loading washout certificate.
Verifying Testing Laboratories Under ISO/IEC 17025 and NAAU Scope Registries
We also audited how enterprises verify external laboratory data. Under FSSC 22000 Additional Requirement 2.5.1(e), all analyses that verify food safety controls (PRP, OPRP, CCP, EMP pathogen swabs, potable water, packaging migration, pesticide residues, mycotoxins, and veterinary drugs) must be performed by testing laboratories accredited to ISO/IEC 17025 or participating in recognized proficiency testing schemes. During the workshop, teams looked up their contracted laboratories in the official registry of the National Accreditation Agency of Ukraine (NAAU) and caught cases where a lab held a general ISO/IEC 17025 certificate, but the specific test method for Listeria monocytogenes or phthalate migration wasn't listed inside its accredited scope annex.
Team Workshop Methodology in Yaremche: Cross-Functional Audit Simulations and Resolving Shop-Floor Conflicts
Why did an offsite workshop in the Carpathians generate faster operational change than standard classroom training? We refused to work from generic templates and instead structured every exercise around the real cross-functional friction that plays out daily between quality assurance, production management, maintenance engineering, and procurement.
Role-Playing Real Conflicts Between Production Uptime and Sanitation
Every food plant faces the same tension: the production manager is measured on shift output and Overall Equipment Effectiveness (OEE), while the Food Safety Team leader demands a 90-minute line shutdown to dismantle a depositor, run a full caustic wash, and swab for peanut protein before switching to an allergen-free batch. Inside the factory, that argument often ends in a rushed wash or a rubber-stamped logbook.
In Yaremche, we seated production supervisors, chief mechanics, procurement specialists, and QA managers at the same table and swapped their roles in simulated FSSC 22000 audits. When a production manager plays the lead auditor and sees firsthand how an unwashed homogenizer dead leg or a torn sifter mesh triggers certificate suspension and halts retail exports, resistance to PRP discipline vanishes. That shared ownership is the foundation of Food Safety Culture required by both GFSI and ISO 22002-100:2025.
Open Engineering Exchange Across Food, Packaging, and Logistics Sectors
The atmosphere in Yaremche was focused, candid, and genuinely enjoyable. Between technical blocks, specialists from dairy plants, meat processors, industrial bakeries, flexible packaging converters, and cold-chain carriers compared practical fixes: which foam stations hold pressure longest, how to rodent-proof loading docks during autumn harvest, and how to structure sampling calendars. Teams didn't just listen to lectures; they tested engineering fixes against their own plant constraints and left with a synchronized action plan.
Photo Report from Ekontrol's Offsite Engineering Practicum in Yaremche
Below is our photo report capturing the working groups, engineering case defenses, ISO 22002-100:2025 matrix reviews, and team discussions during Ekontrol's offsite training practicum in Yaremche on January 28, 2025.
From Training to Certification: Corporate Workshops, Pre-Audit Diagnostics, and 90-Day Implementation with Ekontrol
Training a Food Safety Team delivers real return on investment when workshop decisions turn into measurable engineering and procedural upgrades on the plant floor. Every team leaving our Yaremche practicum returned to their facility with a structured 90-day transition roadmap for ISO 22002:2025 and updated compliance protocols for FSSC 22000, ISO 22000, and HACCP.
The 90-Day Post-Training Engineering Transition Roadmap
Experience across Ekontrol industrial projects shows that asking a single quality manager to rewrite all PRP procedures in a week produces paper-only compliance that collapses during an unannounced audit. Instead, sustainable readiness follows a four-stage engineering cycle:
- Days 1-20: Pre-Training or Post-Training Shop-Floor Diagnostic Audit. Our lead auditors walk your entire production flow alongside your FST, inspecting hygienic zoning,
HVACpressure cascades,CIPreturn loops, floor drains, chemical stores, and packaging warehouses againstISO 22002-100:2025and your sector standard (-1,-4,-5). - Days 21-45: Tailored Corporate Practicum and Documentation Re-Engineering Under Management System Implementation. We run a site-specific workshop built around your exact equipment, eliminate duplicated
PRPinstructions, update your hazard analysis under Clause 8.5 of ISO 22000, and formalize change management under Clause 6.3. - Days 46-75: Instrumental and Accredited Laboratory Validation. Together with your chief engineer and laboratory staff, we validate
CIPcleaning regimes, verify allergen changeover protocols, mapEMPswabbing points across Zones 1-4, and test packaging migration in accredited testing laboratories compliant with ISO/IEC 17025. - Days 76-90: Unannounced Mock Audit, Certification Audit Support, and Ongoing Annual System Support. We conduct a full-scale unannounced stress audit, close root causes using
CAPAmethodology, coach line operators for auditor interviews, and back your team during certification body assessments.
If your facility is preparing for the ISO 22002-100:2025 transition, facing an upcoming FSSC 22000 surveillance or recertification audit, or needs a hands-on offsite or on-site engineering workshop for your Food Safety Team, reach out to Ekontrol specialists via our contact page.
| Ekontrol Corporate Preparation Stage | Implementation Timeline | Plant Team Participants | Engineering and Methodological Scope | Deliverable for Management and Certification Auditors |
|---|---|---|---|---|
| Stage 1. On-Site Pre-Audit Gap Analysis (/diagnostic-audit) | Weeks 1-3 (Days 1-20) | Quality Director, FST Leader, Chief Engineer, Production Manager | Physical inspection of hygienic zoning, HVAC, CIP, drainage, storage, and lab controls against ISO 22002-100:2025 and sector parts (-1, -4, -5) | Photographic gap report, risk heatmap, and prioritized CAPEX/OPEX engineering remediation plan |
| Stage 2. Customized Offsite or On-Site FST Engineering Practicum | Weeks 4-5 (Days 21-35) | Full Food Safety Team, shift supervisors, technologists, procurement leads, internal auditors | Hands-on workshop using your plant blueprints: cross-contamination mapping, allergen validation, EMP Zones 1-4, TACCP and VACCP drills | Trained cross-functional team with personal certificates and agreed dual-standard PRP procedure templates |
| Stage 3. PRP Overhaul and Lab Validation (/implementation and /iso-17025) | Weeks 6-10 (Days 36-75) | FST working group, plant laboratory, mechanical and utilities engineering department | Migration to two-tier SOP architecture, CIP and allergen cleaning validation, EMP and packaging migration testing in ISO/IEC 17025 labs | Updated FSSC 22000 / ISO 22000 documentation suite and complete validation dossier for critical processes |
| Stage 4. Mock Stress Audit, Certification Defense, and Maintenance (/audit-support and /annual-support) | Weeks 11-13 (Days 76-90) and ongoing | Plant leadership, shop-floor operators, Food Safety Team | Unannounced mock FSSC 22000 audit, operator interview coaching, CAPA closure verification, and quarterly surveillance support | Successful certification or surveillance audit with zero critical or major nonconformities and stable compliance |
Measurable Plant Impact from Combining FST Practicums with Ekontrol Diagnostic Audits
Across Ekontrol industrial projects in 2025-2026, manufacturing sites that paired a hands-on FST engineering workshop with a pre-audit shop-floor diagnostic under ISO 22002-100:2025 and its sector standards cut allergen line-changeover downtime by 18-25% and reduced minor nonconformities during FSSC 22000 certification audits by threefold on average.
Book a Custom ISO 22002-100:2025 Corporate Workshop or FSSC 22000 Diagnostic Audit
Ekontrol lead auditors and engineers will tailor a practical training program to your plant processes, run a shop-floor PRP gap analysis, and prepare your Food Safety Team for certification audits.
Request a training or audit proposal